




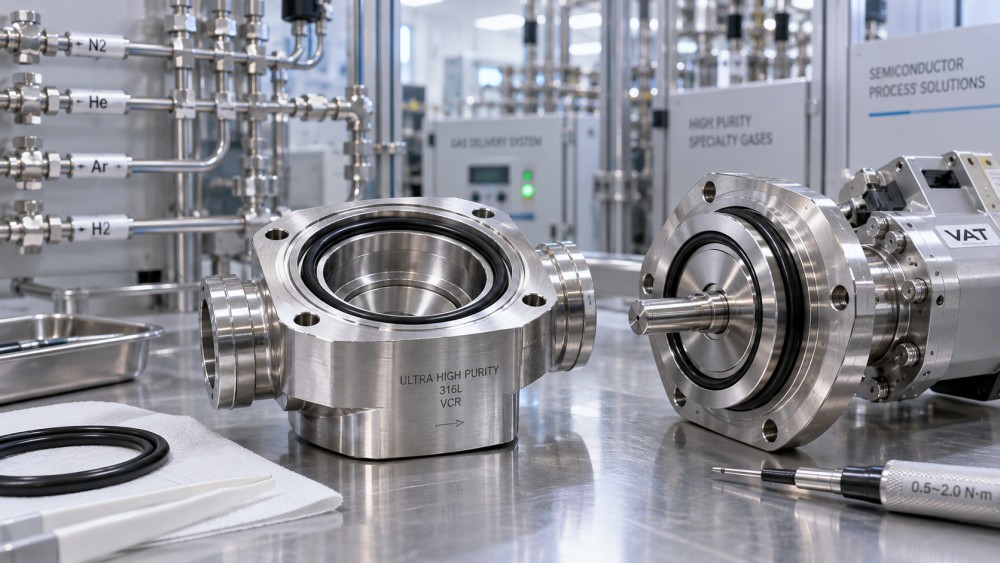
FFKM O-rings merit consideration in semiconductor gas control systems when aggressive process gases, elevated temperatures, or stringent contamination limits exceed the capabilities of conventional elastomers. But a premium material is not automatically the right seal. Performance depends on the specific compound, gas chemistry, thermal cycling, gland design, and leakage requirements—not simply the FFKM designation.
For technical evaluators, the decision is usually practical: will this seal reduce contamination, extend service intervals, or prevent a failure that disrupts production? Answering that question requires examining the actual sealing interface. A valve actuator seal isolated from process gas has very different duties from an O-ring exposed to a heated precursor stream.
Start with the interface: does it need an elastomer at all?
Before comparing FFKM with other elastomers, confirm that an O-ring is appropriate for the connection. Many high-purity gas delivery systems use metal face seals, welded tubing, and diaphragm valves to minimize permeation, outgassing, and process-exposed polymer surfaces. FFKM is not a substitute for those architectures when their performance is required.
Elastomeric seals remain relevant in serviceable valve assemblies, certain regulator and instrument designs, manifold interfaces, and connections between gas delivery equipment and process tools. Even within one component, however, an O-ring may serve as a secondary containment seal rather than the primary process barrier.
The first selection question is therefore not “Which FFKM grade?” but “What does this particular seal contact, contain, and protect?” Review the component drawing and the equipment manufacturer’s approved materials before proposing a substitution. A material upgrade that changes friction, compression, or assembly behavior can compromise an otherwise qualified valve.
When FFKM becomes a strong candidate in semiconductor gas control
Chemical exposure is limiting the existing seal
FFKM, or perfluoroelastomer, combines an elastomeric structure with extensive fluorination, providing broad chemical resistance. It deserves evaluation when a qualified FKM or other conventional elastomer shows swelling, hardening, cracking, or loss of sealing force under the actual process conditions.
That does not make FFKM universally resistant. Compound formulation and cure chemistry matter, particularly with reactive gases, oxidizing environments, and elevated-temperature exposure. A compatibility rating for a chemical family is only a screening tool; it does not establish suitability for every gas mixture or operating condition.
Consider the full exposure sequence, including purge gas, cleaning agents, residual moisture, and reaction products. A seal may tolerate the nominal feed gas yet deteriorate when trapped residues encounter moisture during maintenance. Compatibility must cover the operating cycle, not just the gas listed on the process recipe.
Heat and chemistry act together
Heated delivery lines and precursor-handling equipment can push elastomers beyond their useful sealing range. Some FFKM compounds offer a higher-temperature capability than conventional alternatives, making them candidates where chemical resistance and thermal durability are both necessary.
Use the temperature at the seal location, including heat tracing, startup overshoot, and shutdown conditions. A heater setpoint or bulk gas temperature may not represent the O-ring’s actual exposure.
A published maximum temperature is not a guaranteed service-life rating. Continuous operation near that limit, especially with aggressive chemistry and sustained compression, can produce unacceptable compression set or embrittlement. Thermal cycling also matters: a seal that remains tight when hot may leak after cooling if it has lost elastic recovery.
Seal degradation is creating a contamination risk
In contamination-sensitive applications, the consequence of a seal problem can extend beyond visible leakage. Extractables, outgassing, particles, and process-induced degradation products may affect downstream performance before the seal fails a conventional leak check.
A semiconductor-focused FFKM compound may help address these risks, but “FFKM” alone is not a cleanliness specification. Filler systems, cure residues, post-curing, cleaning, packaging, and handling all influence suitability. A grade optimized for mechanical durability may not be the preferred choice for a particularly sensitive gas path.
Distinguish leakage mechanisms before choosing a material
A failed leak test can make an expensive material change feel urgent. Yet not every leak originates in chemical attack, and FFKM will not correct a damaged gland or an incorrectly assembled joint.
Separate leakage along the sealing interface from permeation through the elastomer. Interface leakage may result from insufficient squeeze, surface damage, contamination, misalignment, or loss of sealing force. Permeation is transport through the material itself; it depends on the gas, compound, temperature, pressure differential, and seal geometry.
FFKM should not be assumed to have the lowest permeability for every gas. Where the allowable gas load is extremely low, a metal-sealed design may be more appropriate than changing elastomer families.
Vacuum service adds another distinction: inward leakage, permeation, and outgassing can all contribute to the measured gas load. A helium leak result also depends on the test method and timing. Define the acceptance criterion and procedure together so that suppliers and equipment teams are evaluating the same behavior.
A material comparison that supports an actual decision
The following comparison is a screening framework, not an approval list. The exact compound and component design determine whether any option is acceptable.
The important distinction is between choosing a material and choosing a sealing system. PTFE and metal seals are generally not drop-in replacements for an O-ring. Likewise, replacing one elastomer with FFKM requires checking the gland and component—not merely matching the nominal size.
What to request before approving an FFKM compound
A useful supplier discussion starts with a defined operating envelope. Provide the gas identities and mixtures, pressure and vacuum conditions, temperature profile, exposure duration, purge sequence, and expected maintenance interval. Include abnormal but credible conditions, such as a heating excursion or delayed purge.
Then request evidence tied to the proposed compound:
- Application-relevant compatibility: Exposure conditions, duration, and observed changes in dimensions, hardness, mechanical properties, or sealing performance.
- Thermal sealing behavior: Compression-set data and, where available, compression stress-relaxation information relevant to the duty.
- Contamination characteristics: Applicable outgassing, extractables, particle, and trace-element data, with the test methods identified.
- Manufacturing controls: Compound identification, dimensional tolerances, lot traceability, cleaning, packaging, and change-notification practices.
- Component approval: Confirmation that the equipment manufacturer permits the exact grade and dimensions in the intended location.
Ask what each report actually establishes. An immersion test can help screen chemical resistance, but it does not automatically predict dry-gas performance under pressure. A room-temperature material test says little about sealing-force retention after repeated hot operation.
For toxic, pyrophoric, strongly oxidizing, or otherwise hazardous gases, obtain application-specific review from the equipment manufacturer and responsible safety specialists. General chemical resistance does not establish ignition resistance, safe failure behavior, or suitability for hazardous-gas service.
Check the gland before blaming the compound
Review squeeze, gland fill, stretch, tolerances, surface finish, and extrusion clearance against the proposed material and operating conditions. Thermal expansion and chemical swelling can reduce available gland volume. Hardness and pressure differential influence extrusion risk.
Dynamic applications require additional attention to friction, wear, and actuation behavior. An O-ring that performs well in a static manifold joint may be unsuitable in a repeatedly moving valve interface. Unapproved lubricants can also introduce contamination or compatibility problems, even when the seal itself is correctly specified.
Validate the sequence the seal will actually experience
A short, steady-state leak test is a starting point—not a complete qualification. The revealing condition may be the first cold restart after prolonged hot exposure, or a pressure transition after the seal has taken compression set.
Build the qualification around the real service sequence:
- Establish a baseline. Record dimensions, condition, assembly details, and initial leakage under a defined procedure.
- Apply representative exposure. Include process chemistry, operating temperature, pressure differential, and relevant purge conditions using appropriately controlled facilities.
- Exercise operating transitions. Reproduce meaningful heating, cooling, pressure, vacuum, and actuation cycles.
- Repeat functional checks. Assess leakage, valve operation, and contamination indicators relevant to the application.
- Inspect after disassembly. Examine deformation, cracking, deposits, wear, and evidence of extrusion or installation damage.
Set acceptance criteria before testing. “No visible damage” is insufficient if the governing requirement is gas purity or sealing after cooldown. Conversely, a cosmetic change should be interpreted against functional criteria rather than treated automatically as failure.
Accelerated testing needs care: increasing temperature may change the degradation mechanism rather than simply shorten the test. Use results to support an engineering judgment, not to claim an unsupported service-life multiplier.
Make the cost decision at the failure-consequence level
FFKM is easier to justify where a seal-related intervention requires shutdown, decontamination, extended purging, component replacement, and requalification. In those locations, acquisition price is only one part of lifecycle cost. Maintenance labor, lost availability, troubleshooting, and potential contamination consequences may matter much more.
Still, anticipated savings should be supported by qualification results or relevant service history. If the existing approved seal already lasts through the planned maintenance interval without contamination or leakage problems, FFKM may add cost without delivering a useful improvement.
Procurement should also protect the approved specification. Similar-looking O-rings are not necessarily interchangeable. Retain the exact compound designation, dimensions, cleanliness requirements, packaging, and traceability in purchasing records. A generic order for “FFKM O-rings” leaves too much room for unintended substitution.
Use FFKM in semiconductor gas control when a specific, qualified compound solves a demonstrated chemical, thermal, or contamination limitation in an elastomer-compatible interface. Keep a qualified alternative where it already meets the duty, and consider a different sealing architecture where permeation, purity, or safety requirements demand it. The strongest selection is not the most expensive material—it is the one whose performance remains defensible through operation, maintenance, and the next restart.
Want to dive deeper into these market dynamics, or need data-driven support for your next business move? Drop a line below and let the analysts at PCTS provide customized insights.
We respect your privacy. Your information is strictly confidential.
Related News
- 00
0000-00
How sealing technology reduces contamination in semiconductor manufacturing - 00
0000-00
Where to install vibration sensors on rotating machinery - 00
0000-00
NTSB Probe Finds Boeing Warned of MD-11 Engine Bearing Risk Years Earlier - 00
0000-00
How to size pneumatic grippers for packaging system integration - 00
0000-00
How to size alloy steel power transmission chains for heavy loads
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.